R$ 40 (Brazilian reais) versus R$ 180. Two connector quotes for the same application, and the four-and-a-half-fold difference seems to settle the matter. It does not, because price is the smallest share of a connection's cost. The largest is the failure it can cause, and that share sits in another spreadsheet, in another department: the price is in purchasing, the downtime is in maintenance, and nobody adds the two together.
In my assessment, this mismatch is one of the most common forms of waste in industry, precisely because it does not show up as anyone's mistake; it shows up as “maintenance cost”. The tool that brings the two spreadsheets together is total cost of ownership. Applied to connections, it gives a complete calculation, a break-even point that is easy to defend and a path to the decision.
What total cost of ownership (TCO) is
TCO (total cost of ownership) is everything an item costs over its life: purchase, installation, maintenance, failures and replacement. The question stops being “how much does this connector cost?” and becomes “how much will this connection point cost me over the next five years?”.
For connections, this reasoning makes even more sense than for machines, for a simple reason: the component's price is small, and the cost of the failure it can cause is large. When the gap between price and consequence is that wide, deciding on price means deciding on the smaller part of the bill.
The rule of thumb known as 1-10-100 sums up the logic: what costs 1 to prevent in design costs in the order of 10 to correct at installation and 100 when it fails in operation. It is not measured data; it is an order of magnitude, and it explains why TPM treats specification as maintenance prevention (or early equipment management): the cheapest reliability is the one decided before purchase.
What goes into the total cost of a connection
Each TCO component is linked to a technical characteristic of the connection. This is where specification turns into money:
| Component | What to consider | Technical characteristic that matters |
|---|---|---|
| Acquisition | Connector, cable gland, accessories, cable | Material, degree of protection, number of poles |
| Installation | Technician hours, tools, assembly errors and rework | Number of components, co-moulded seal, pre-wired versions |
| Inspection and maintenance | Time to inspect, retighten, clean, disconnect and reconnect | Re-inspectable connection, plug and socket |
| Failures | Probability of failure × cost of each failure | Suitability for the environment: water, chemicals, heat, condensation, impact |
| Replacement | Replacement at end of service life and spare parts in stock | Resistance to ageing, UV, ozone and salt mist |
The formula, in one line:
TCO = acquisition + installation + maintenance over the period + (expected failures × cost per failure)
The cost per failure follows the calculation presented in Industrial electrical connections and productivity: downtime hours × line cost per hour + labour + materials + scrap. The hourly cost comes from the machine-hour calculation.
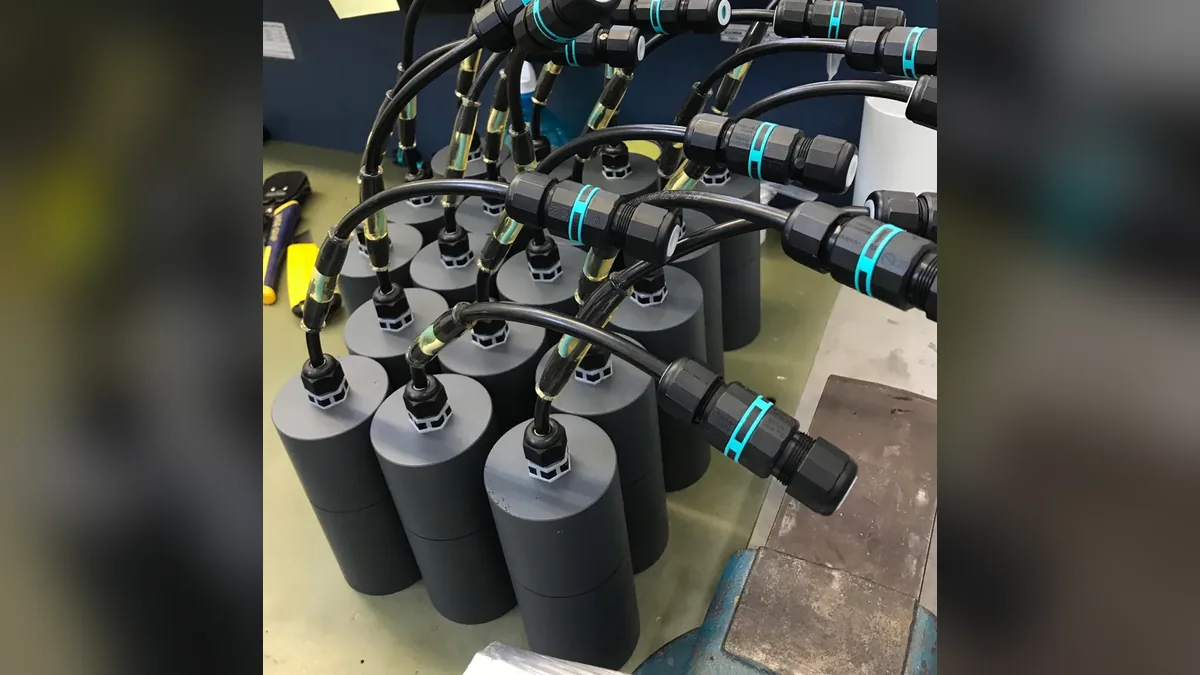
In the method Techno do Brasil presented at Mundo SENAI (described in the guide to Techno do Brasil's technology), several design decisions act directly on these components. The co-moulded seal, according to the company, reduces the number of components, speeds up installation and lowers assembly errors; the pre-wired versions, according to the catalogue, leave the factory with electrical and mechanical tests done; the watertight plug and socket reduces the time needed to replace a motor or sensor.
From an engineering standpoint, this is what makes the approach a differentiator in TCO terms. Every interface eliminated (a loose O-ring, a splice made in the field) is one less failure mode in a DFMEA, and it lowers the probability of failure by design, not through the care of whoever does the assembly. The disconnectable connection reduces MTTR (mean time to repair) structurally. And the material tests, for ozone, salt mist and UV, address the ageing that shortens service life and that the IP test, carried out on a new unit, does not measure. What TCO does is put a price on these three advantages.
Worked example: conventional or robust?
| Item (per point) | Option A: conventional connection | Option B: robust connection |
|---|---|---|
| Acquisition | R$ 40 | R$ 180 |
| Installation | 1.5 h × R$ 80 = R$ 120 | 0.5 h × R$ 80 = R$ 40 |
| Initial subtotal | R$ 160 | R$ 220 |
| Probability of failure per year | 4% | 1% |
| Expected failures in 5 years | 0.20 | 0.05 |
| Expected cost of failures | 0.20 × R$ 9,000 = R$ 1,800 | 0.05 × R$ 9,000 = R$ 450 |
| 5-year TCO | R$ 1,960 | R$ 670 |
Look at what happened. Option B is R$ 140 more expensive to buy, but the faster installation recovers R$ 80 of that difference on day one. That leaves R$ 60 more in initial investment, and the total cost falls by R$ 1,290 per point.
The break-even point
The most useful question for the decision is a different one: how much does option B need to improve to pay for itself? The extra R$ 60 pays for itself if it prevents 60 ÷ 9,000 ≈ 0.0067 failures per point over 5 years. In shop-floor language: it only has to prevent one failure for every 150 points installed. That number is usually much easier to defend in a meeting than any probability estimate.
What if downtime costs less?
Redo the calculation for a simpler line, at R$ 2,000 per hour. The cost per failure drops to R$ 3,000. Option A comes to R$ 160 + 0.20 × R$ 3,000 = R$ 760; option B, to R$ 220 + 0.05 × R$ 3,000 = R$ 370. The break-even point rises to 60 ÷ 3,000 = 0.02, or one failure prevented for every 50 points. The conclusion changes in size, but not in direction. The general rule: the more expensive the downtime, the smaller the improvement needed to justify the robust connection.
At the scale of a line
A line with 120 connection points in a humid environment, keeping the assumptions of the first scenario, would have 24 expected failures in 5 years with option A and 6 with option B. The combined TCO would be R$ 235,200 versus R$ 80,400. That is 18 fewer stoppages, and each of them is a shift that did not have to be replanned.
The same assumption shows the effect of series reliability. If a circuit has 20 of these points, the probability of at least one failure in the year is 1 − 0.9620 ≈ 56% with option A and 1 − 0.9920 ≈ 18% with option B. In a series system, improving each point and reducing the number of points are the only two levers, and both feed straight into TCO.
The calculation holds between options that meet the same technical requirements (current, voltage, poles, cross-section, cable diameter, temperature and degree of protection) and is only confirmed if the robust option actually eliminates the cause of the failures. That is why the probabilities should come from your plant's history and from the manufacturer's technical data.
The cost the spreadsheet does not show
The table above is conservative, because it leaves out costs that exist and are rarely counted:
- Diagnosing intermittent faults. Moisture-related failures come and go. Before getting to the connection, the team usually tests the sensor, the PLC card and the whole cable, and sometimes replaces parts that were fine. The mechanism is explained in Condensation and water ingress in connections.
- Spare parts inventory. Many different connector families for the same function mean more items in the storeroom. Standardising the specification reduces the variety of spare parts and MRO.
- Difficult access. A connection in a buried box, in an underground chamber or high up on a structure costs more to inspect and repair, sometimes requiring access equipment and a permit to work.
- Safety. In guard-locking switches and emergency stop buttons, a failing connection is a safeguard that does not respond. That cost is not measured in reais per hour.
- Real service life. In the pitch lighting case shown by Techno, the installer reports opening the connector, in an inspection chamber that fills with water when it rains, four years after installation, and finding no trace of water. It is this kind of inspection that grounds a service-life estimate in facts. Other cases are in Connection cases in harsh environments.
How to take the numbers to purchasing and senior management
In projects I have followed, the technical argument rarely won on its own. What changes the decision is putting, on the same sheet, the price purchasing sees and the downtime production feels. A practical roadmap:
- Gather the actual failures from the last year by cause and component, with a Pareto chart. Include the “back to normal, nothing replaced” work orders.
- Calculate the cost per failure using the hourly cost of the affected line.
- Build the TCO for both options and, above all, the break-even point.
- Propose a pilot on one machine or a group of points, with MTBF and MTTR measured before and after.
- Also measure installation time, which is usually the quickest saving to prove.
- Standardise what the pilot confirms, in the purchasing specification and in the TPM inspection plan.
For the specification itself, use the checklist for choosing industrial electrical connectors, which follows Techno's three-step method: environment, cable and weak points.
From connection to competitiveness
Reducing repeat failures is not just a maintenance saving. The effect spreads across the operation:
- Capacity without investment. Downtime hours avoided are productive hours recovered, which shows up directly in OEE and TEEP.
- Predictability. A line that does not stop unexpectedly meets deadlines, and meeting deadlines is a sales argument.
- Quality. Fewer unstable readings from sensors and weighing scales mean less rework and scrap.
- A team free to improve. The technician who is not redoing the same splice can carry out planned maintenance and improvement work.
- Faster expansions. Standardised, quick-to-install connections shorten the assembly of new lines.
In Lean, this has a name: tackling waste at the source, not after it has turned into downtime. The article Lean and waste in component selection develops this idea.
Industrial competitiveness is usually discussed in terms of exchange rates, taxes and major investments. All of that matters. But part of it is decided in quotes of R$ 40 and R$ 180, by people who do not always have the complete calculation in hand. Putting that calculation on the table is one of the cheapest improvements a plant can make.
Frequently asked questions
What is the TCO of an electrical connection?
It is the total cost of ownership of the connection point: purchase, installation, maintenance, expected failures and replacement over a period, usually 3 to 10 years.
Does a more expensive connection always pay off?
No. It pays off when it actually reduces failures or installation time under your conditions. The break-even point shows how many failures the more expensive option needs to prevent to pay for itself.
How do I estimate the probability of failure of a connection?
From your plant's work order history, broken down by environment and connection type, and from the manufacturer's technical data. Without history, use ranges (optimistic, likely, pessimistic) and see whether the decision changes.
Does installation cost make a difference to TCO?
Yes, especially in projects with many points. Solutions with fewer components, a co-moulded seal or a pre-assembled cable reduce technician hours and assembly errors, and that saving shows up on day one.
Which metrics should I track after the switch?
Number of failures per connection, equipment MTBF and MTTR, downtime hours, installation time and the effect on OEE availability.
In this series
- Techno do Brasil: electrical connection technology (series guide)
- Industrial electrical connections and productivity
- How to choose industrial electrical connectors
- IP66, IP68 and IP69K: what they mean
- Condensation and water ingress in connections
- Industrial connections and TPM: reliability
- Lean and waste in component selection
- Connection cases in harsh environments
- Total cost of industrial connections (TCO)
Sources
- Techno. Aplicações Complicadas e Hostis (“Complicated and Hostile Applications”, technical presentation in Portuguese), given by Mário Adinolfi on 6 November 2026 at Mundo SENAI, Marechal Cândido Rondon (PR).
- Techno. General Catalogue (CATGENIT102024), Portuguese edition.
- Installer's report on the inspection after 4 years (Instagram).
- IEC 60300-3-3: Dependability management, Application guide, Life cycle costing.
- Lean Enterprise Institute: what is Lean.
- ABRAMAN: Brazilian Association of Maintenance and Asset Management.
Save this address: Manufatura Enxuta is your lean manufacturing school. Come back whenever you need to study, with complete articles, a visual map and reliable sources. Follow one of the study paths or check the A–Z glossary.
Explore the technology at the source
This series explains the technology behind connections and its effect on waste. For the technical data of each item, consult the catalogue and the data sheets on the official Techno do Brasil website.
Visit the official website
About the author
Vagner Soares
Specialist in Lean Manufacturing and Behavioural Management
More than 20 years in the automotive and metalworking industries (GM and Dana), and a Lean Manufacturing specialist since 2006. SENAI instructor and mentor in the Brasil Mais Produtivo programme, with consulting, training and audits in more than 50 companies, bringing together quality, productivity and people development.


