What one piece flow is
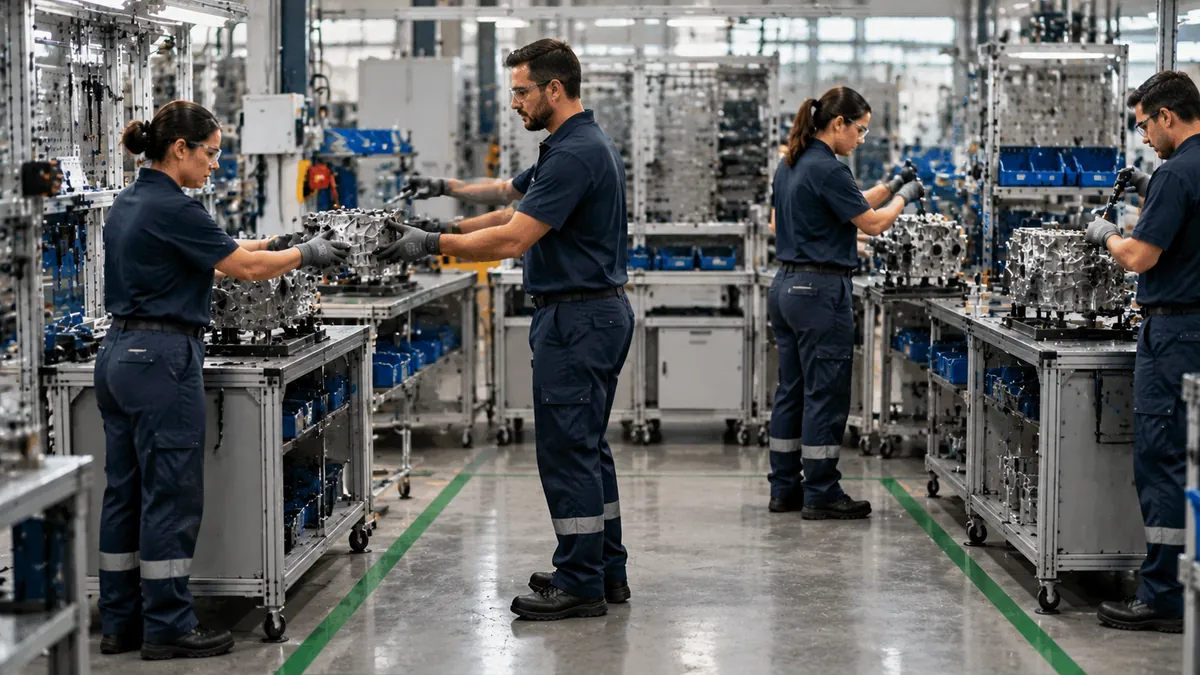
One piece flow means making and moving one unit at a time from one process to the next, with no batches and no inventory between them. A part enters the next step only when the previous one releases it.
The main gain is lead time: the first part leaves after adding up only the time of each step, instead of waiting for the whole batch. Because the next station sees a defect within minutes, scrap also drops.
Visual map: batch of one versus large batches in lead time
The map compares a batch of 10 with single-piece flow using the same example as this article, and shows the formula and the conditions for use.

Example: 3 stations of 1 minute, 10 parts
Three processes in sequence, each taking 1 minute per part, and an order of 10 parts. In batch mode, each station processes all 10 parts before passing them on. In single-piece flow, each part moves on as soon as it is done.
| Metric | Batch of 10 | One piece flow |
|---|---|---|
| First part done | 3 × 10 × 1 = 30 min | 3 × 1 = 3 min |
| Last part done | 30 min | (3 + 10 − 1) × 1 = 12 min |
| Average exit of the 10 parts | 30 min | (3 + 4 + … + 12) ÷ 10 = 7.5 min |
| Work in process (steady state) | 1 per minute × 30 min = 30 | 1 per minute × 3 min = 3 |
| Parts hit by a defect at station 1 | up to 10 | up to 2 |
Capacity is the same, 1 part per minute. What changes is how much time and material sit idle along the way.
The lead time math
Batch: LT = m × Q × t | One piece flow: LT = (m + Q − 1) × t
Here m is the number of stations, Q the batch size and t the time per part (equal at all stations). Work in process follows Little's law: WIP = output rate × throughput time.
| Stations (m) | Batch Q = 10: m × Q × t | One piece flow: (m + Q − 1) × t |
|---|---|---|
| 3 | 30 min | 12 min |
| 5 | 50 min | 14 min |
| 8 | 80 min | 17 min |
The more steps, the bigger the advantage of single-piece flow. It delivers this only when cycle times are similar.
The pace is set by the slowest station
If station 3 takes 1.5 minutes and the others take 1, part n leaves at 2 + 1.5 × n. The tenth part leaves at 17 minutes, versus 35 minutes in batch mode (10 + 10 + 15). Still better, but station 3 caps output at 0.67 parts per minute. That is why one piece flow calls for line balancing against takt time: cycle times should sit close to takt, with no station far above the rest. To tell the concepts apart, see cycle time, takt time and lead time.
How to implement it in 6 steps
- Pick a product family with a similar routing, using the value stream map.
- Measure the real time of each step and calculate the takt for the order.
- Rearrange stations in process sequence, close together. The typical layout is the U-shaped cell.
- Balance the work across operators until no step runs far above takt.
- Cut changeovers and stoppages with SMED and basic maintenance, because with no buffer any stop halts the flow.
- Build quality in at the source with poka-yoke and stopping the station on a defect, in the spirit of jidoka.
Start with a pilot cell, record before and after lead time, work in process and scrap, and only then replicate.
When to use it and when not to
| Condition | Does one piece flow work? | What to do |
|---|---|---|
| Cycle times close to takt | Yes | Apply directly |
| Long changeover | Not yet | Cut it with SMED; use small batches |
| Batch process (oven, bath, cure) | No | Use the equipment's minimum batch, with flow before and after |
| Unstable machine with frequent stops | No | Stabilize first (TPM) |
| Many variants and different routings | Partly | Group families; level with heijunka |
| Stations far apart or in different buildings | Partly | Tighten the layout or use continuous flow with a buffer |
When single-piece flow is not possible, use continuous flow with small batches and link separate processes with pull production. One piece flow is the goal, not a rule for every process.
Common mistakes and limits
- Forcing flow with unbalanced times: the operator at the fast station waits while the slow station builds a queue.
- Ignoring changeovers: with long changeovers, the capacity loss outweighs the lead time gain.
- Removing inventory before stabilizing: the first machine or quality failure stops the whole cell.
- Confusing single-piece flow with single-piece transport: moving one part at a time over long distances adds motion.
- Judging only by cost per hour: local efficiency drops, but the gain is in throughput time, inventory and quality.
- Sizing with no slack: with no stock, the cell depends on attendance, tooling and material at the point of use.
Frequently asked questions
What is one piece flow?
Making and moving one part at a time between steps, with no batches and no intermediate inventory.
How is it different from continuous flow?
Continuous flow is the broader idea: parts keep moving. One piece flow is the ideal form, with a transfer batch of 1.
How much does lead time drop in the example?
From 30 minutes to 12 minutes for the last part, and the first part leaves at 3 minutes instead of 30.
Does it suit every process?
No. Batch processes, long changeovers and unstable machines call for small batches or fixes first.
Does it reduce productivity?
In the example, capacity is the same, 1 part per minute. Local idle time shows up because the inventory that hid it is gone.
Do I need a U-shaped cell?
Not required, but it is the most common layout because it brings stations together and lets you vary the number of operators.
Sources
- OHNO, T. Toyota Production System: Beyond Large-Scale Production. Productivity Press, 1988.
- WOMACK, J. P.; JONES, D. T. Lean Thinking. Free Press, 2003.
- ROTHER, M.; HARRIS, R. Creating Continuous Flow. Lean Enterprise Institute, 2001.
- HOPP, W. J.; SPEARMAN, M. L. Factory Physics. Waveland Press.
- LITTLE, J. D. C. A proof for the queuing formula L = λW. Operations Research, v. 9, n. 3, 1961.
Keep studying: trusted sources and links
Save this address: Manufatura Enxuta is your school for lean manufacturing. Come back whenever you need to study, with a complete article, a visual map and trusted sources. Follow one of the learning paths or check the A–Z glossary.
Want real pull production?
Download the free pull production e-book, with kanban, supermarkets and leveling.
Download the e-book
About the author
Lean Manufacturing & Behavioral Management Specialist
Over 20 years in the automotive and metalworking industries (GM and Dana), Lean Manufacturing practitioner since 2006. SENAI instructor and mentor in Brazil’s Brasil Mais Produtivo program, delivering consulting, training and audits for 50+ companies, combining quality, productivity and people development.