What a kaizen event is
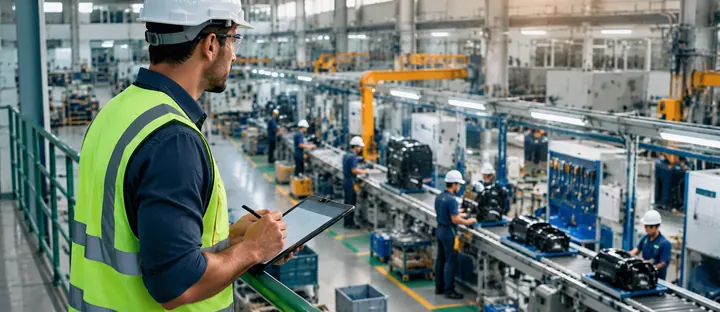
A kaizen event (also called a kaizen blitz or rapid improvement event) is an intensive effort, usually 3 to 5 days, in which a cross-functional team analyzes one process, tests changes right at the workplace and leaves the new method running by the end of the week. Unlike daily continuous improvement, it concentrates people, time and decision authority on a single target.
It is one way of applying kaizen, close to what flow kaizen describes. The key point: when the event ends, the change is implemented and measured, not just proposed in a report.
Kaizen event visual map
The map summarizes the three phases, the five-day schedule and the result of the example in this article.

Before the event: what must be ready
The event is won or lost in the two weeks before it. Without preparation, day one is spent hunting for data.
- Narrow scope: one process, one cell or one product family. "Reduce lead time in assembly cell X" works; "improve the plant" does not.
- Measurable target: for example, reduce WIP and lead time without adding people.
- Sponsor: a manager who releases the team, approves layout changes and attends the final readout.
- Team of 6 to 8: operators from the area, maintenance, quality, process engineering and one person from outside the process who questions what everyone considers normal.
- Current-state data: daily volume, cycle times, work in process, scrap, layout and photos or video of the workstation.
- Logistics: a room near the area, test material, tape, cardboard, stopwatches and maintenance support to move benches.
Capture it all in a one-page charter: problem, scope, target, constraints (what cannot change) and members. An A3 report works well for this.
The 5-day schedule
| Day | Focus | Deliverables |
|---|---|---|
| 1 | Train and understand | Basics (waste, takt), trip to the gemba, current-state measurement |
| 2 | Analyze and generate ideas | Flow map, spaghetti diagram, causes via 5 Whys, prioritized idea list |
| 3 | Implement | Layout change, kits, visual signals, first real trial |
| 4 | Test and adjust | Post-change measurement, fixes, written standard work |
| 5 | Standardize and present | Training for all shifts, 30-day plan, management readout |
The rule for day 3 is "cardboard before bolts": simulate benches and racks with temporary material, validate with the operators and only then fix things in place.
Worked example: an assembly cell (fictional case)
A cell serves 120 units per day. Before the event it had 4 operators, 240 units in process and 48 m of walking per cycle because of an island layout. By Little's law, lead time is work in process divided by throughput:
Lead time = WIP ÷ throughput = 240 ÷ 120 = 2.0 days
The team joined the benches into a U-shaped cell, created component kits and capped WIP between stations. Result on Thursday, at the same demand of 120 units per day:
| Metric | Before | After | Change |
|---|---|---|---|
| WIP (units) | 240 | 60 | −75% |
| Lead time (days) | 2.0 | 0.5 (60 ÷ 120) | −75% |
| Walking per cycle (m) | 48 | 18 | −62.5% |
| Operators | 4 | 3 | −1 person |
| Units per operator per day | 120 ÷ 4 = 30 | 120 ÷ 3 = 40 | +33.3% |
The numbers are illustrative. What is worth copying is the method: measure before, measure after, on the same demand base. The freed operator was reassigned, not laid off; agreeing on that before the event prevents resistance. See also how to calculate lead time.
When to use it and when not to
| Use when | Avoid when |
|---|---|
| The problem is clear and local (flow, layout, changeover) | The cause is unknown and needs weeks of data |
| There is a sponsor and the team is released | People can only join "when there is spare time" |
| The fix relies on quick physical changes | The fix needs a long purchase or an engineering project |
| The area needs a visible win to build trust | The area is in a staffing or delivery crisis |
Good targets: changeover time with SMED, cell layout, line replenishment and information flow. Complex quality problems call for a longer PDCA cycle.
After the event: sustaining the gain
The biggest loss from a kaizen event is sliding back to the old state within 60 days. To prevent it:
- Open-items list with owner and due date (a 5W2H board works), reviewed at 30, 60 and 90 days.
- Short audit of the new standard by the leader, at the gemba, twice a week during the first month.
- Visible metric at the cell, updated by the people who run it.
- Training for the other shifts before the week ends, not after.
- Change management: explain the reason and listen to objections; see change management.
Common mistakes
- Scope too big: the team ends the week with ideas and no implementation.
- No operators on the team: the solution looks good on paper and is rejected at the station.
- Too many ideas, too few trials: the event is for testing, not debating.
- No baseline: without it the gain cannot be proven.
- Treating it as a one-off: without a daily improvement routine, the gain fades.
Frequently asked questions
What is a kaizen event?
An intensive effort of a few days, with a cross-functional team, to improve a specific process and leave the change implemented at the end of the event.
How long does a kaizen event last?
Usually 3 to 5 days, plus preparation in the preceding weeks and follow-up at 30 to 90 days.
Who should take part?
Six to eight people: operators from the area, maintenance, quality, engineering and one participant from outside the process, backed by a sponsoring manager.
What is the difference between a kaizen blitz and daily kaizen?
A blitz concentrates team and time on one target to get a large change quickly. Daily kaizen involves everyone in small, constant improvements.
How do you measure the result?
With before and after metrics on the same demand: WIP, lead time, walking distance, output per operator and scrap.
What if the gain is lost afterwards?
Review the standard with the operators, strengthen leader audits and keep the metric visible; usually the routine is missing, not the idea.
Sources
- IMAI, Masaaki. Kaizen: The Key to Japan's Competitive Success. New York: Random House, 1986.
- LARAIA, Anthony C.; MOODY, Patricia E.; HALL, Robert W. The Kaizen Blitz: Accelerating Breakthroughs in Productivity and Performance. Wiley, 1999.
- ROTHER, Mike; SHOOK, John. Learning to See. Lean Enterprise Institute.
- LIKER, Jeffrey K. The Toyota Way. McGraw-Hill, 2004.
Keep studying: trusted sources and links
- Lean Enterprise Institute: Lean Lexicon, Kaizen
- Lean Enterprise Institute: What is Lean?
- Wikipedia: Kaizen
Save this address: Manufatura Enxuta is your school for lean manufacturing. Come back whenever you need to study, with a complete article, a visual map and trusted sources. Follow one of the learning paths or check the A–Z glossary.
Want the tools ready to use?
Download the free "Problem Solving Kit" e-book, with PDCA, A3, 5 Whys and Ishikawa.
Download the e-book
About the author
Lean Manufacturing & Behavioral Management Specialist
Over 20 years in the automotive and metalworking industries (GM and Dana), Lean Manufacturing practitioner since 2006. SENAI instructor and mentor in Brazil’s Brasil Mais Produtivo program, delivering consulting, training and audits for 50+ companies, combining quality, productivity and people development.