Kaizen works on a small scale
Kaizen means change for the better, made step by step and by everyone. In practice, most improvements are small: a shelf moved, a jig, a label that prevents confusion.
The five examples below are illustrative. They were designed to show the reasoning and do not report cases from real companies. To learn the method, read Kaizen: how to implement continuous improvement. For the implementation roadmap, see how to implement kaizen in production.
One point comes before all the examples: kaizen is not a specialist's project, it is the habit of the people who work at the workstation. That is why the improvements below are small, cheap, and testable within a few days. If an idea requires budget approval, it has probably already outgrown an individual kaizen.
How to read each example
All the examples follow the same structure, which resembles the PDCA cycle:
- Problem: what bothers the people who work at the workstation.
- Idea: the proposed change.
- Action: what was done.
- Verification: how to know whether it worked.
Notice that the idea always comes from the person doing the work. That is the central point of kaizen.
In every case, one final question is worth asking: what keeps the problem from coming back? The answer is the new standard. Without it, the example is just a good idea that lasted a few weeks.
Example 1: a tool that is always out of place
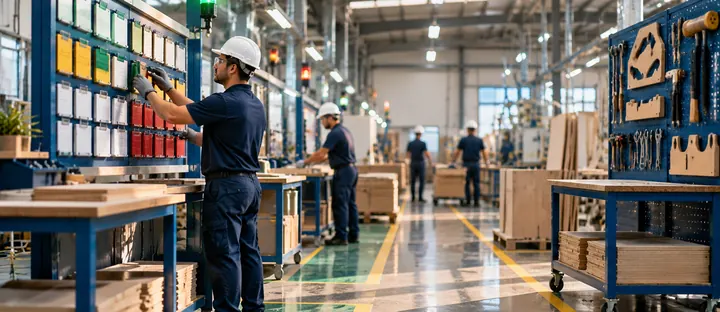
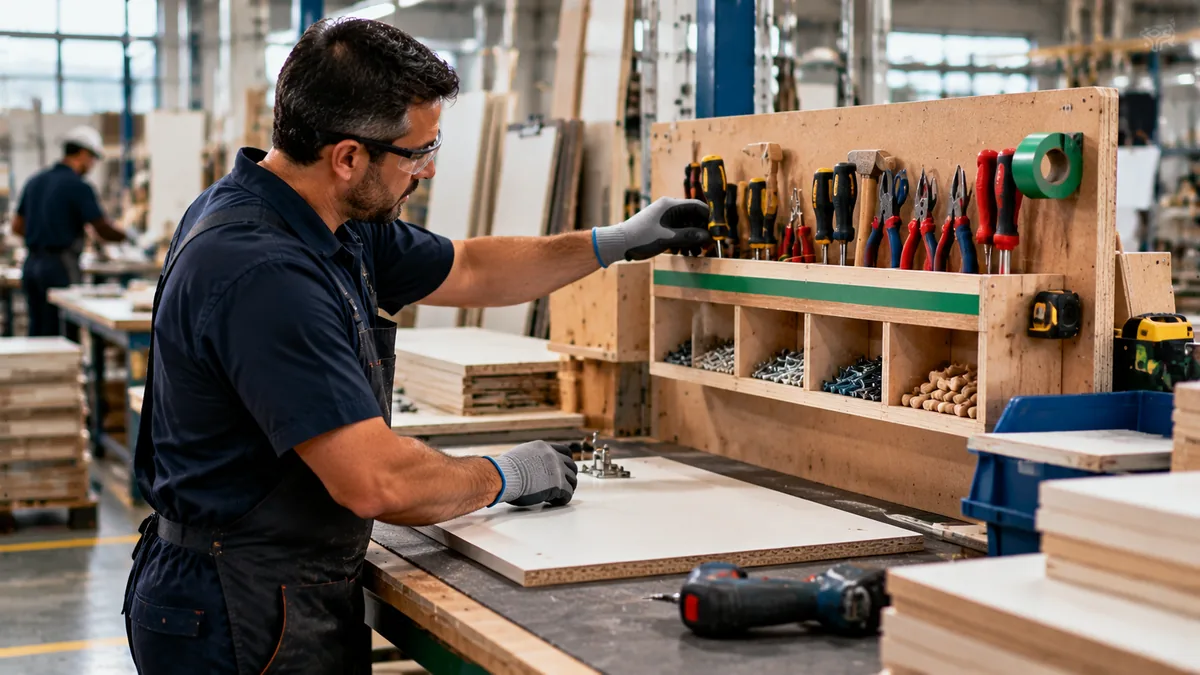
Problem: the assembler spends part of the shift looking for the torque wrench. Idea: give the tool a fixed address. Action: a panel with the silhouette (shadow) of the tool, at hand height. Verification: count how many times per shift the tool is searched for, before and after, over one week.
It is a direct application of 5S. Low cost and immediate results.
Practical detail: the person who uses the tool should take part in choosing where the panel goes. The placement that looks logical to the designer is not always the most comfortable for the person doing the work. Test the position for one shift before fixing it permanently.
Example 2: a part fitted backwards
Problem: a symmetrical part is occasionally assembled upside down. Idea: make the inversion impossible. Action: add a guide pin to the fixture so that only the correct side seats. Verification: track assembly defects per week.
This type of solution is known as poka-yoke: the error no longer depends on attention.
Example 3: too much walking to resupply
Problem: the operator walks to the storeroom several times per shift to fetch screws. Idea: bring the material to the workstation. Action: screw bins with two compartments; when the first one empties, a signal calls for replenishment. Verification: count trips per shift.
The logic is replenishment by consumption. Those who want to go deeper will find the concept in kanban.
Watch the size of the stock at the workstation. The two-compartment bin should hold only a short period's consumption, otherwise the solution turns into a small uncontrolled inventory. Set the quantity based on actual consumption and adjust after a few days.
Example 4: information that does not arrive
Problem: the night shift does not know which orders are urgent. Idea: make the information visible. Action: a production board with colors by priority, updated at the end of each shift. Verification: count how many urgent orders are late in a month.
The principle is in visual management: the status of the work is visible without asking anyone.
The board has to be simple. Three colors, one owner, and one update time are enough. Complex boards take more time to maintain than they save, and end up abandoned.
Example 5: a machine that stops without warning
Problem: a press stops several times a week and nobody knows why. Idea: record every stop. Action: a log sheet with time, duration, and perceived cause, filled in by the operator. Verification: after four weeks, group the causes and attack the most frequent one with the 5 Whys.
The recurrence is analyzed with root cause analysis and, where appropriate, through the autonomous maintenance of TPM.
This example shows a rule of kaizen: before solving, see. Many teams rush to a solution without knowing the frequency or the cause of the problem. Four weeks of records may reveal that most stops come from a single cause, and then the effort is concentrated where it pays off.
Next step
Choose one annoyance at your workstation and fill in the four lines: problem, idea, action, and verification. Test it for a week. If it worked, write down the new way of working. If not, adjust the idea.
To structure a broader program, see 5 continuous improvement techniques and the article on the 3 types of kaizen.
A tip for running it: record each test on a one-page sheet with the date, owner, what changed, and the measured number. After a month you will have a small knowledge base for the area, useful for training newcomers and for justifying larger investments when a simple idea is no longer enough.
Also remember to celebrate the result with the people who did the work. One minute of recognition at the start-of-shift meeting costs nothing and sustains the habit better than any campaign.
Frequently asked questions
Are the five examples real company cases?
No. They are illustrative scenarios, created to show the reasoning of kaizen without attributing results to any company.
Does every kaizen need investment?
No. Most improvements are low-cost and come from the ideas of the people who do the work.
How do I know whether a kaizen worked?
Measure a simple quantity before and after, such as trips per shift, defects per week, or minutes of downtime.
Who should propose the improvements?
Mainly the people who perform the activity, with support from supervision to remove obstacles.
Keep studying
Sources
- IMAI, M. Kaizen: A Estratégia para o Sucesso Competitivo. São Paulo: IMAM.
- Lean Enterprise Institute. Lean Lexicon: Kaizen. https://www.lean.org/lexicon-terms/kaizen/
- Lean Enterprise Institute. Lean Lexicon: PDCA. https://www.lean.org/lexicon-terms/pdca/
Keep studying: trusted sources and links
Save this address: Manufatura Enxuta is your school for lean manufacturing. Come back whenever you need to study, with a complete article, a visual map and trusted sources. Follow one of the learning paths or check the A–Z glossary.
Want the tools ready to use?
Download the free "Problem-Solving Kit" e-book, with PDCA, A3, 5 Whys, and Ishikawa.
Download the e-book
About the author
Lean Manufacturing & Behavioral Management Specialist
Over 20 years in the automotive and metalworking industries (GM and Dana), Lean Manufacturing practitioner since 2006. SENAI instructor and mentor in Brazil’s Brasil Mais Produtivo program, delivering consulting, training and audits for 50+ companies, combining quality, productivity and people development.