- What an SQDCM board is
- Visual map of the SQDCM board
- The five columns and what to measure in each
- Color rule: when it is green, yellow or red
- Weekly example from an assembly cell
- From red to action
- The 10-minute stand-up at the board
- How to set up the board in five steps
- Common mistakes
- Frequently asked questions
What an SQDCM board is
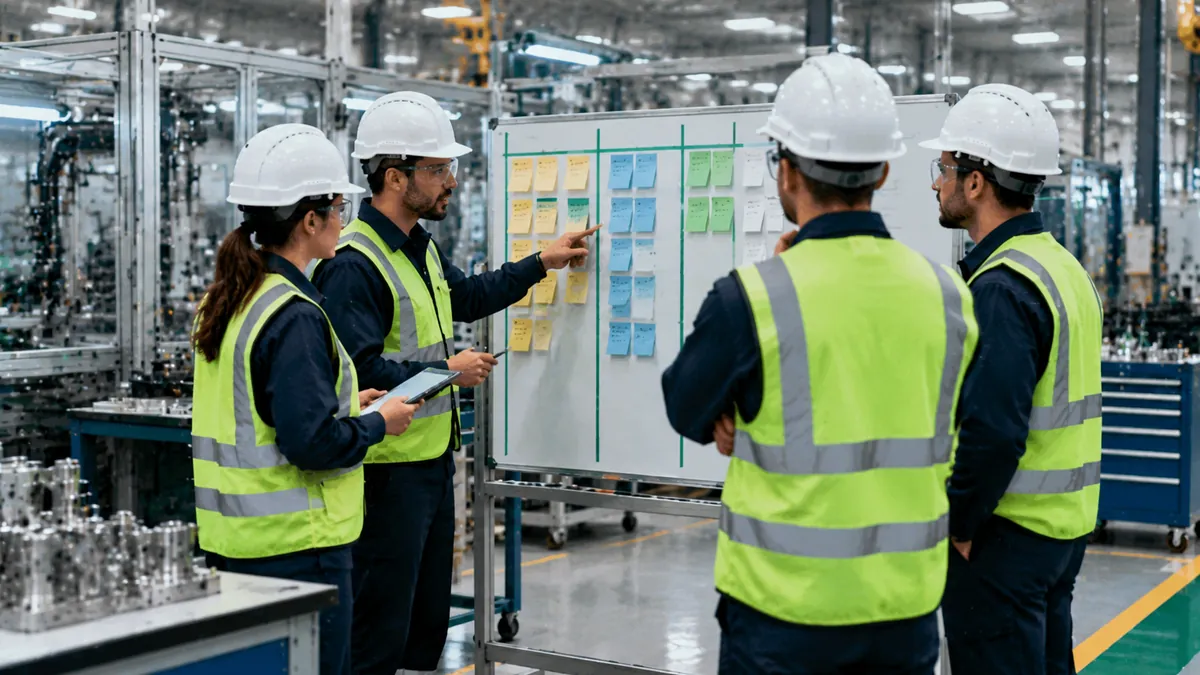
An SQDCM board is a visual management board, updated daily at the workplace itself, that tracks five dimensions: Safety, Quality, Delivery, Cost and Morale. Each column shows a target, the day's result and, when the target is missed, the open action with an owner and a due date.
The SQDC acronym comes from daily management practice at automakers and their suppliers; the "M" for morale is the most common lean manufacturing variant. Order matters: safety comes first and is never traded for volume.
Visual map of the SQDCM board
The map summarizes the five columns, the color rule, the weekly example and the 10-minute meeting script.

The five columns and what to measure in each
| Letter | Question of the day | Typical metrics |
|---|---|---|
| S: Safety | Did anyone get hurt, or nearly? | Days without a lost-time accident, near misses reported, open unsafe conditions |
| Q: Quality | Did we get it right the first time? | First pass yield (FPY), scrap, rework, customer complaints |
| D: Delivery | Did we hit today's plan? | Actual ÷ planned, hour by hour; stoppages and their reasons |
| C: Cost | Did we spend more than planned? | Overtime hours, scrapped parts, material usage, hours per unit |
| M: Morale | Is the team well and involved? | Absenteeism, improvement suggestions per week, skills matrix, team mood |
Pick one to three metrics per column. A board with twelve metrics per letter becomes wallpaper: nobody reads it and nobody acts. For quality data use FPY and RTY; for the delivery column, actual ÷ planned is enough.
Color rule: when it is green, yellow or red
Define the rule before hanging the board, so nobody argues about the color. A simple rule used on shop floors:
- Green: target met.
- Yellow: up to 1 percentage point below target.
- Red: more than 1 point below target (or any lost-time accident).
Every red needs a recorded action: what, who and by when. Red without an action is decoration, and it is the most common failure of visual management.
Weekly example from an assembly cell
Fictional example: a cell with 12 operators and a takt time of 1 minute per unit (480 line minutes, 480 units per day, 60 per hour). The week's result:
| Day | Planned | Actual | Delivery (%) |
|---|---|---|---|
| Monday | 480 | 480 | 100 |
| Tuesday | 480 | 456 | 95 |
| Wednesday | 480 | 432 | 90 |
| Thursday | 480 | 480 | 100 |
| Friday | 480 | 468 | 97.5 |
| Week | 2,400 | 2,316 | 96.5 |
Delivery = actual ÷ planned = 2,316 ÷ 2,400 = 96.5%
Of the 2,316 parts, 2,247 came out good the first time: FPY = 2,247 ÷ 2,316 = 97.0%, with 69 parts reworked or scrapped. Against the cell's targets, the week's board reads:
| Column | Metric | Target | Actual | Color |
|---|---|---|---|---|
| S | Days without lost-time accident | continuous | 142 | Green |
| Q | FPY | 98% | 97.0% | Yellow (1.0 point below) |
| D | Weekly delivery | 98% | 96.5% | Red (1.5 points below) |
| C | Overtime hours in the week | up to 10 h | 14 h | Red (40% above) |
| M | Absenteeism (1 absence in 60 person-days) | up to 3% | 1.7% | Green |
Two reds, and they are linked: on Wednesday the cell built 432 instead of 480, which is 48 units short. At 60 parts per hour, that is 48 minutes of lost production, later recovered with overtime. The board shows the connection without any report.
From red to action
In the example, the team leader writes on the board's action line, in 5W2H style:
- Problem: Wednesday, 48 min of downtime from a missing component at station 4.
- Likely cause: supermarket replenishment with no set time.
- Action: define a replenishment route and schedule.
- Owner and due date: internal logistics, by Friday.
- Check: next week's delivery and stoppages for missing material.
If the action is beyond the cell leader's reach, it moves up to the next tier, as explained in lean daily management and tier meetings.
The 10-minute stand-up at the board
The board only works with a fixed routine. A lean script, standing, at the start of the shift:
- Safety (1 min): accidents, near misses and the day's risk.
- Quality (2 min): yesterday's defects and where they were found.
- Delivery (2 min): yesterday's result and today's plan, including expected stoppages.
- Cost (1 min): overtime and scrap.
- Morale (1 min): absences, suggestions, recognition.
- Actions (3 min): open, chase and close, with an owner and a date.
The cell leader runs it; operators update their own column. Add a supervisor gemba walk to check that what is on the board is what happens at the workstation.
How to set up the board in five steps
- Pick a pilot cell with a willing leader and data that already exists.
- Define one to three metrics per letter and a target for each, together with the team.
- Standardize the update: who writes, at what time, with which pen, in what format (daily bar chart or hour-by-hour table).
- Place it in the work flow, where the team passes and can stand around it, not in the manager's office.
- Review after 30 days: cut what nobody uses, add what generated action. Then roll out to other cells.
If the plant already runs a management room, the cell's SQDCM feeds the Obeya with the same metrics, only consolidated.
Common mistakes
- A pretty, stale board: data a week late. The board is worth today's data.
- Too many metrics, or metrics the team cannot influence.
- Red without an action, or an action with no due date and no owner.
- Data filled in by the office instead of the team: no owner, no engagement.
- Using the board to punish: people start hiding problems and painting everything green.
- Forgetting Morale or treating it as decoration; it is the gauge of whether the routine is sustainable.
Frequently asked questions
What does SQDCM stand for?
Safety, Quality, Delivery, Cost and Morale: the five dimensions tracked on the daily board.
What is the difference between SQDC and SQDCM?
The M adds team morale (absenteeism, suggestions, climate). Everything else is the same; many companies use the version with M.
How long should the meeting at the board last?
Ten to fifteen minutes, standing, at the start of the shift, always at the same time.
Who should update the board?
The cell team itself, each person on their own column. The leader runs the meeting but does not fill in everything alone.
How many metrics per column?
One to three. The board must be readable in seconds; detail belongs in separate analyses.
Does SQDCM replace the Obeya?
No. It is the cell's board; the Obeya consolidates metrics from several areas for management.
Sources
- MANN, David. Creating a Lean Culture: Tools to Sustain Lean Conversions. 3rd ed. Boca Raton: CRC Press, 2014.
- LIKER, Jeffrey K. The Toyota Way: 14 Management Principles from the World's Greatest Manufacturer. New York: McGraw-Hill, 2004.
- GREIF, Michel. The Visual Factory: Building Participation Through Shared Information. Portland: Productivity Press, 1991.
- GALSWORTH, Gwendolyn D. Visual Workplace, Visual Thinking. Portland: Visual-Lean Enterprise Press, 1997.
Keep studying: trusted sources and links
Save this address: Manufatura Enxuta is your school for lean manufacturing. Come back whenever you need to study, with a complete article, a visual map and trusted sources. Follow one of the learning paths or check the A–Z glossary.
Want to measure what really matters?
Download the free e-book on performance indicators and track the losses in your operation.
Download the e-book
About the author
Lean Manufacturing & Behavioral Management Specialist
Over 20 years in the automotive and metalworking industries (GM and Dana), Lean Manufacturing practitioner since 2006. SENAI instructor and mentor in Brazil’s Brasil Mais Produtivo program, delivering consulting, training and audits for 50+ companies, combining quality, productivity and people development.